Disclosure: This post contains affiliate links and I will be compensated if you make a purchase after clicking through my links. Learn More
Many people want to weld stainless steel because it is strong, rust-resistant, and looks clean. MIG welding is a popular way to join stainless steel. MIG stands for Metal Inert Gas. This method uses a wire electrode and shielding gas to make a strong bond.
Stainless steel is different from mild steel or aluminum, so you need special steps to get a good result. If you make mistakes, you may see rust, weak joints, or distortion. This guide explains everything you need to know about MIG welding stainless steel.
You will learn how to choose the right tools, set up your machine, prepare your metal, and finish your weld. Even if you are new to welding, you can get professional results by following these steps.
Why Mig Weld Stainless Steel?
MIG welding stainless steel is popular in many fields. People use it in kitchens, food factories, hospitals, cars, and art projects. Stainless steel stays clean and resists rust, which is important for hygiene and strength. MIG welding is faster and easier than TIG welding for many jobs.
It is good for joining thin sheets or large pieces. MIG also creates less spatter than stick welding.
MIG welding is easy to learn and works well for beginners. It uses a spool of wire and a gas bottle. You pull the trigger, and the machine does most of the work. The process allows you to weld long seams without stopping often.
If you need to weld stainless steel at home or in your shop, MIG is a strong choice.
Key Differences: Stainless Steel Vs. Other Metals
Stainless steel is not the same as mild steel or aluminum. It has unique features that affect how you weld.
- Heat sensitivity: Stainless steel warps easily if you use too much heat. It loses strength and color.
- Thermal expansion: Stainless steel expands more than mild steel when hot. Gaps and distortion can happen if you do not control heat.
- Chromium content: Stainless steel has chromium, which fights rust. Overheating can burn off chromium and cause rust spots.
- Weld pool fluidity: The molten metal behaves differently. The pool is not as fluid as mild steel, so you must move the torch smoothly.
Knowing these differences helps you set up your MIG welder the right way and avoid common problems.
Types Of Stainless Steel You Can Mig Weld
Not all stainless steels are the same. Here are the main types you may need to weld:
- Austenitic stainless steel (300 series): Grades like 304 and 316 are common. They are easy to weld and resist corrosion well. Most kitchen and food equipment uses these grades.
- Ferritic stainless steel (400 series): Grades like 409 and 430 are magnetic and less expensive. They are harder to weld and can crack if you use the wrong filler.
- Martensitic stainless steel: Grades like 410 and 420 are harder and used for knives and tools. They are difficult to weld and need special care.
Austenitic grades are the best choice for beginners. Always check the grade before you buy wire or gas.
Choosing The Right Mig Welder
Not every MIG welder can handle stainless steel. Here’s what you need to consider:
- Power: Pick a MIG welder with enough amps for your material thickness. For thin sheets (1–3 mm), a 140–180 amp machine is enough. For thicker plates, go higher.
- Voltage settings: Variable voltage helps you fine-tune your weld.
- Wire feed speed control: You need to adjust this to avoid burn-through or weak welds.
- Gas compatibility: Your welder must work with argon and CO2 mixes (see below).
- Spool gun support: If you plan to weld aluminum too, this feature helps.
Check the manual before you buy. Some small MIG welders are only for mild steel.
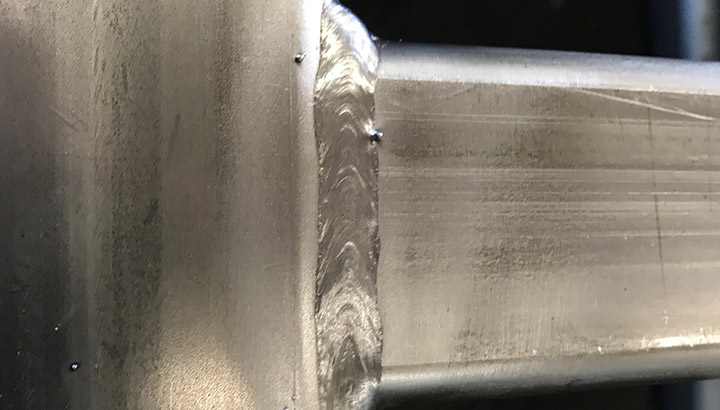
Credit: www.millerwelds.com
Essential Equipment And Tools
You need more than just a MIG welder. Here is a list of tools and safety gear for welding stainless steel:
- MIG welding machine
- Stainless steel MIG wire (ER308L, ER316L, etc.)
- Shielding gas (argon/CO2 mix)
- Wire brush (stainless steel bristles only)
- Angle grinder (with flap disk for stainless steel)
- Clamps and magnets (to hold pieces in place)
- Welding helmet (auto-darkening is best)
- Gloves (leather, heat-resistant)
- Jacket or apron (protects your body)
- Cutting tools (if you need to size metal)
- Measuring tools (tape, square, marker)
Do not use normal steel brushes or disks on stainless steel. They can leave particles that cause rust.
Selecting The Right Mig Wire
Choosing the right wire is critical. The wrong wire can cause cracks, rust, or weak welds. Here are common options:
- ER308L: Use for 304 stainless steel. It is the most common.
- ER316L: Use for 316 stainless steel. It resists chemicals and saltwater.
- ER309L: Use to join stainless steel to mild steel.
- Diameter: 0.030″ (0.8 mm) or 0.035″ (0.9 mm) is common for thin to medium thickness.
Check the metal grade before picking your wire. Always use wire that matches or exceeds the corrosion resistance of your base metal.
Best Shielding Gas For Mig Welding Stainless Steel
Shielding gas protects your weld from air and keeps it clean. The right mix makes a big difference.
Most people use a tri-mix gas for stainless steel:
- 90% helium
- 7.5% argon
- 2.5% CO2
Some shops use 98% argon with 2% CO2 for thin stainless steel. Pure CO2 can cause too much heat and spatter.
Helium makes the arc hotter and helps the weld pool flow. Argon keeps the arc stable. CO2 helps with penetration.
Never use 100% CO2 for stainless steel. It can cause oxidation and lower quality.
Comparison Of Shielding Gas Mixes
| Gas Mix | Use Case | Pros | Cons |
|---|---|---|---|
| 90% He / 7.5% Ar / 2.5% CO2 | General stainless steel MIG welding | Low spatter, good penetration | More expensive |
| 98% Ar / 2% CO2 | Thin stainless steel sheets | Clean welds, less burn-through | Lower penetration |
| 100% CO2 | Mild steel only | Cheap, deep penetration | Poor for stainless, oxidizes weld |
Preparing Stainless Steel For Mig Welding
Good preparation makes a big difference in weld quality. Stainless steel is sensitive to dirt, oil, and rust. If you weld without cleaning, you will see porosity, cracks, or rust later.
- Clean with a stainless steel wire brush. Never use a carbon steel brush. Even small bits of iron can cause rust stains.
- Remove oil and grease with acetone or alcohol. Wipe the surface with a clean rag.
- Grind the edges if needed. Use a flap disk or sanding pad for stainless steel.
- Fit-up the joints. Use clamps or magnets to hold pieces together. Leave a small gap (about 1 mm) for butt joints. This helps the weld penetrate fully.
- Check for coatings. Some stainless steel has a plastic film. Remove it before welding.
Never touch the cleaned surface with bare hands. Sweat can leave salt that causes rust.
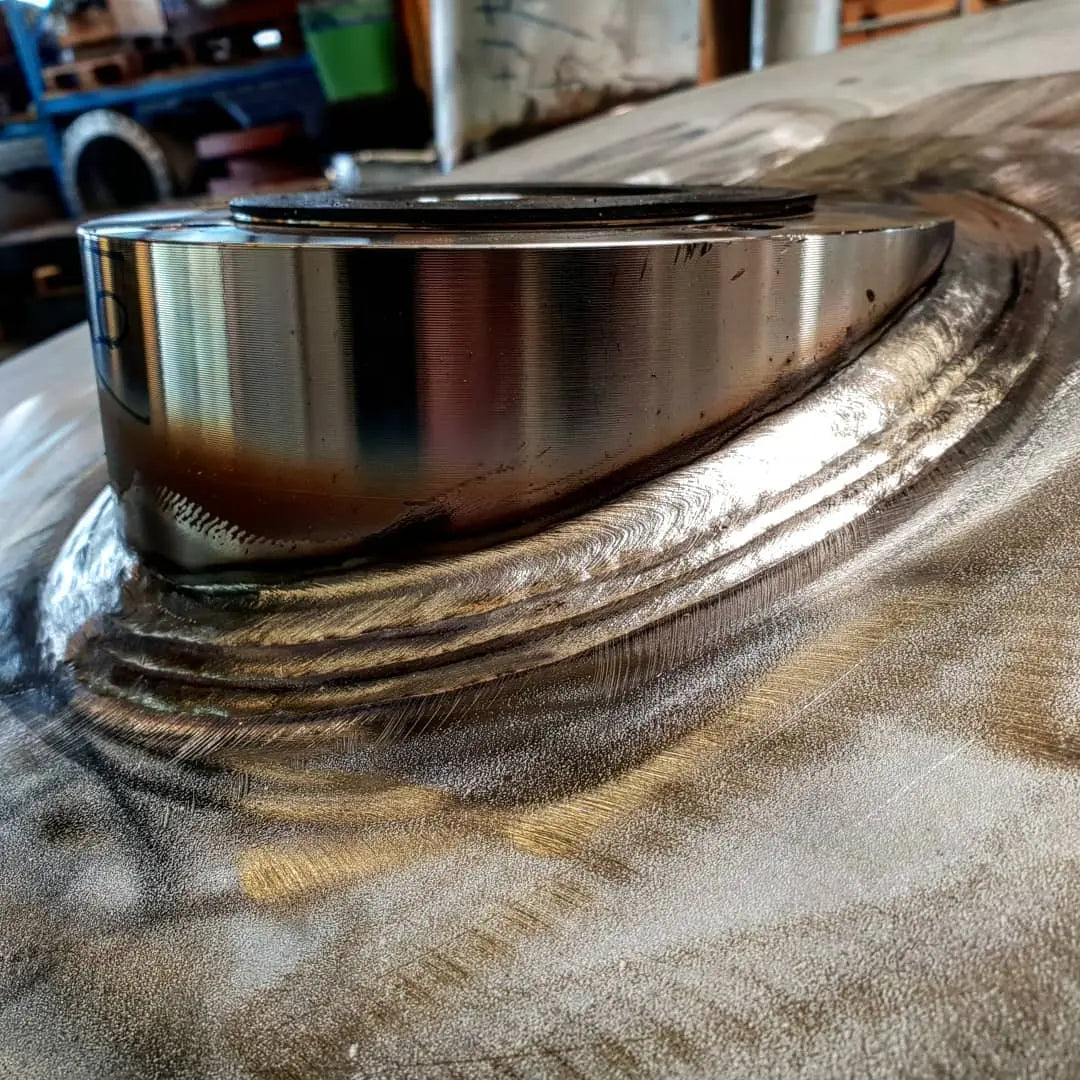
Credit: tooliom.com
Setting Up Your Mig Welder For Stainless Steel
Correct machine settings are key for a strong, neat weld. Here is how to set up your MIG welder:
- Polarity: Use DC Electrode Positive (DCEP, also called reverse polarity).
- Voltage: Start with the settings suggested in your welder manual. Adjust up or down based on your test weld.
- Wire feed speed: Set to match your voltage and wire size. Too fast causes spatter; too slow makes the arc unstable.
- Gas flow rate: Use 15–20 cubic feet per hour (CFH). Too low lets air in; too high can pull in air from around the nozzle.
- Inductance (if adjustable): Higher inductance gives a smoother arc for stainless steel.
Example Mig Settings For Stainless Steel (using 0.030″ Wire)
| Material Thickness | Voltage (V) | Wire Feed Speed (ipm) | Gas Flow (CFH) |
|---|---|---|---|
| 18 gauge (1.2 mm) | 16–17 | 190–200 | 15–20 |
| 16 gauge (1.6 mm) | 17–18 | 210–220 | 15–20 |
| 1/8″ (3.2 mm) | 20–21 | 260–280 | 18–22 |
Always do a test weld on scrap metal before you start your project. Adjust settings until the bead looks flat and even with little spatter.
How To Mig Weld Stainless Steel: Step-by-step
Here is a full process for MIG welding stainless steel. Each step matters for a strong, clean weld.
1. Prepare Your Workspace
Work in a well-ventilated area. Stainless steel fumes can be harmful. Remove flammable items. Set up your tools and clamps.
2. Clean And Fit The Pieces
Clean both sides of your weld joint. Use a stainless steel wire brush and acetone. Dry the metal with a lint-free cloth. Fit the pieces tightly, using clamps to hold them.
3. Install The Right Wire And Gas
Load the correct stainless steel MIG wire. Set up your gas bottle with the right mix (tri-mix or argon/CO2). Check hose connections for leaks.
4. Set Your Machine
Adjust voltage, wire feed speed, and gas flow. Use your test piece to find the best settings. The arc should sound steady, not popping or hissing.
5. Tack Weld The Joints
Tack weld at the corners to hold everything in place. Place tacks every few inches. This prevents movement and warping.
6. Weld In Short Passes
Weld small sections (called “stitch welding”). Move the torch smoothly and steadily. Do not dwell in one spot; you may overheat and warp the metal. Let the metal cool between passes if needed.
7. Control Your Torch Angle
Keep the torch at about a 10–15 degree angle from vertical, pushing the weld pool. This gives good gas coverage and a flat bead.
8. Watch Your Travel Speed
Move at a steady speed. Too slow causes burn-through and discoloration; too fast gives poor fusion. Aim for a flat, shiny bead.
9. Clean Between Passes
If you need more than one layer, clean each pass with a stainless steel brush. This removes slag and keeps the weld strong.
10. Inspect And Finish
Check your weld for cracks, undercut, or porosity. If you see problems, grind out the bad weld and redo. Clean the finished weld with a brush and, if needed, a light acid pickling paste to restore color.
Common Mistakes And How To Avoid Them
Beginners make the same mistakes when MIG welding stainless steel. Here is how to avoid them:
- Using the wrong wire or gas: This causes rust or cracks. Always double-check both.
- Not cleaning the base metal: Dirt or iron particles cause rust. Clean with proper tools.
- Too much heat: Causes warping, discoloration, and weak welds. Use short passes and let the metal cool.
- Wrong torch angle: Leads to poor gas coverage and spatter. Keep a steady hand.
- Moving too fast or slow: Fast speed gives weak welds, slow speed causes burn-through.
- Not checking fit-up: Gaps or misalignment cause uneven welds. Clamp carefully.
Two less-known tips:
- Always use dedicated tools for stainless steel. Even a small amount of carbon steel can ruin the corrosion resistance.
- Let the metal cool between passes. Rushing leads to heat buildup and distortion.
Finishing And Cleaning Welded Stainless Steel
A strong weld is not the end. Stainless steel needs a clean finish for best looks and performance.
- Wire brush: Use a stainless steel brush to remove discoloration.
- Flap disk: Smooth the weld bead if you want a flush finish.
- Pickling paste: For food-grade or visible parts, use a pickling paste. This removes heat tint and restores corrosion resistance. Always wear gloves and rinse well.
- Passivation: For best rust resistance, use a passivation solution. This rebuilds the chromium oxide layer. It is important for food and medical uses.
Cleaning is not just about looks. It keeps stainless steel strong and rust-free.
Safety Tips For Mig Welding Stainless Steel
Welding is dangerous if you ignore safety rules. Stainless steel fumes can cause illness. Always take these steps:
- Use a respirator or weld in a well-ventilated area. Fumes contain chromium and nickel.
- Wear gloves, helmet, and long sleeves to protect from sparks and UV rays.
- Keep a fire extinguisher nearby.
- Do not touch hot metal with bare hands.
- Check your gas bottles and hoses for leaks.
- Avoid welding near flammable items.
Never weld stainless steel without proper protection. Even short exposure to fumes can be harmful.
Troubleshooting Mig Welding Stainless Steel
Even with practice, problems can happen. Here is how to fix common issues:
Porosity (holes In Weld)
- Cause: Dirty base metal, wrong gas, or draft.
- Fix: Clean metal, check gas flow, shield from wind.
Cracking
- Cause: Wrong wire, high heat, poor fit-up.
- Fix: Use correct wire, lower voltage, fit pieces tightly.
Excessive Spatter
- Cause: Wire feed too high, wrong gas, or arc length.
- Fix: Lower wire speed, check gas mix, keep tip close.
Discoloration (blue Or Brown Weld)
- Cause: Too much heat or poor gas coverage.
- Fix: Reduce heat, increase travel speed, check gas.
Weak Welds
- Cause: Too fast travel, not enough penetration.
- Fix: Slow down, use correct settings.
Mig Vs. Tig Welding For Stainless Steel
Many people ask if MIG or TIG is better for stainless steel. Both have pros and cons.
| Process | Speed | Skill Needed | Finish Quality | Best For |
|---|---|---|---|---|
| MIG Welding | Fast | Easy | Good | Large projects, beginners |
| TIG Welding | Slow | Hard | Excellent | Thin, detailed work |
MIG welding is faster and easier to learn. TIG welding gives a neater finish and more control but is slower. For most jobs, MIG is a strong choice.
Practical Tips For Better Mig Welds On Stainless Steel
You can improve your results with these tips:
- Do a test weld on scrap before starting your main project.
- Keep your stickout short (about 10–15 mm). This gives better gas coverage.
- Use pulse settings if your machine has them. Pulse welding reduces heat and warping.
- Let the work cool naturally. Do not quench in water; it can cause cracking.
- Mark joints with a marker before cleaning. You will not lose your layout.
- Weld from the center out on long seams to control distortion.
- Store your wire and gas in a dry place. Moisture can cause rust or bad welds.
Many beginners miss that even small mistakes (wrong brush, poor fit-up, or rushing) can cause rust weeks later. Patience and careful prep make a big difference.

Credit: yeswelder.com
Applications For Mig Welded Stainless Steel
You can use MIG welded stainless steel in:
- Food processing equipment
- Restaurant kitchens
- Handrails and furniture
- Automotive exhausts
- Art and sculpture
- Medical tools
- Brewing tanks
Stainless steel is strong and clean. MIG welding lets you build everything from art to machines.
Frequently Asked Questions
What Is The Best Shielding Gas For Mig Welding Stainless Steel?
The best shielding gas is a tri-mix of 90% helium, 7.5% argon, and 2.5% CO2. Some people use 98% argon and 2% CO2 for thin sheets. Never use pure CO2. The right gas prevents rust and gives a clean weld.
Can I Mig Weld Stainless Steel With My Regular Mild Steel Wire?
No. Mild steel wire will not match the corrosion resistance of stainless steel. It can cause rust and weak joints. Always use stainless MIG wire (ER308L, ER316L) that matches your base metal.
Why Does My Stainless Steel Weld Turn Blue Or Brown?
This color means overheating or poor gas coverage. Too much heat burns the chromium in the steel and causes discoloration. Lower your voltage, move faster, and check your gas flow.
Is Mig Welding Stainless Steel As Strong As Tig Welding?
Both methods can make strong welds if done right. TIG welding gives a neater look and more control on thin parts. MIG welding is faster and easier for most jobs and is strong enough for many uses.
Do I Need To Clean Stainless Steel After Welding?
Yes. Cleaning removes heat tint and restores corrosion resistance. Use a stainless steel brush, pickling paste, or passivation solution. This step is important for food, medical, or outdoor use.
For more details about stainless steel grades and welding, you can check this Wikipedia page on stainless steel.
Welding stainless steel with MIG is simple if you follow the right steps. Choose the correct wire, clean your parts, set your machine, and weld with care. With practice, you will get strong, rust-free results that last for years.