Disclosure: This post contains affiliate links and I will be compensated if you make a purchase after clicking through my links. Learn More
Welding stainless steel with TIG (Tungsten Inert Gas) can give you beautiful, strong joints. But if you see a rough, gray, or crusty surface on the back of your weld, you have a problem called sugaring. This problem makes the weld weak and ugly. Many new TIG welders face this issue, and even experienced welders can struggle with it on thin or tricky pieces.
Sugaring, also called oxidation or granulation, happens when hot stainless steel reacts with air. It is not just a cosmetic issue. Sugared welds can crack, rust, and fail over time. In industries like food, chemical, and medical work, sugaring is a serious safety risk.
Stopping sugaring is possible once you understand why it happens and how to prevent it. This guide explains the causes, dangers, and proven methods to stop sugaring when TIG welding stainless steel. You’ll learn techniques, equipment adjustments, and real examples that help you weld cleaner and stronger joints every time.
What Is Sugaring And Why Does It Matter?
Sugaring is the rough, black, or gray crust that forms on the back side of a stainless steel weld. It looks like burned sugar, so welders call it “sugaring.” This happens when the back of the weld gets too hot and touches air, causing oxidation.
Sugaring is not just ugly. It can cause:
- Cracks that weaken the weld
- Rust and corrosion, even on stainless steel
- Contamination in pipes or tanks for food, medicine, or chemicals
- Failed weld tests in industries with strict quality rules
Many codes, like ASME and AWS, do not allow sugaring. If you weld for business, shops may reject your work if they see sugaring.
Why Does Sugaring Happen?
Sugaring starts when the protective chromium in stainless steel reacts with oxygen in the air at high heat. This reaction makes rough oxides that are hard to remove. TIG welding heats both sides of the steel—if air touches the hot back side, you get sugaring.
Key reasons why sugaring happens:
- Not enough shielding gas on the back side of the weld (purge gas)
- Too much heat from high welding current or slow travel speed
- Poor fit-up between the pieces, letting air reach the weld root
- Dirty surfaces that burn and cause more oxidation
- Wrong type or flow of shielding gas
Understanding these reasons helps you fix the real cause, not just the result.
How To Stop Sugaring When Tig Welding Stainless Steel
You can avoid sugaring by controlling heat, protecting the weld from air, and keeping everything clean. Here are the most effective ways:
1. Use Proper Back Purging
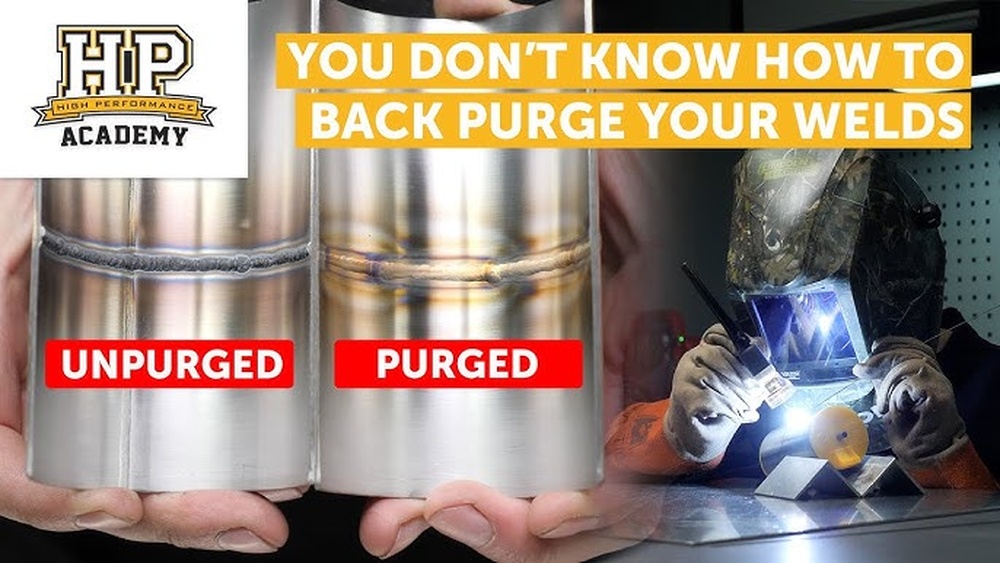
The single most important step is back purging. This means flooding the back side of the weld with an inert gas like argon to keep out air.
How to do it:
- Seal the inside of the pipe or plate with tape, clay, or dams
- Connect an argon line to fill the space behind the weld
- Use about 5-10 CFH (cubic feet per hour) of argon for small pipes, more for large spaces
- Purge the area before you start welding and keep the gas flowing until the weld cools
Tip: Use a purge monitor (oxygen meter) to check if the oxygen level is below 0.1%. This ensures clean shielding.
Common Back Purging Mistakes
- Using too little flow—air sneaks in
- Stopping the purge too soon—the weld is still hot
- Not sealing the ends—leaks let in air
- Using the wrong gas—do not use CO₂ or nitrogen for stainless
Example: A welder uses painter’s tape to seal pipe ends and fills with argon. He welds, but gets sugaring because he did not check for leaks. The tape lifted slightly, letting air in.
2. Adjust Tig Welding Parameters
Too much heat makes sugaring worse. Adjust your settings for stainless:
- Lower the amperage: Use only enough current to get a smooth weld pool
- Keep travel speed steady: Move at a pace that avoids excess heat build-up
- Use a smaller tungsten: 1/16″ (1.6mm) works well for thin stainless
- Set the gas flow right: 15-20 CFH for the torch side
Data Example:
| Parameter | Recommended Setting | Effect on Sugaring |
|---|---|---|
| Amperage (1/16″ steel) | 45-70A | Less heat, less sugaring |
| Travel Speed | 2-4 in/min | Faster means less heat input |
| Torch Gas Flow | 15-20 CFH | Good protection, less oxidation |
Tip: If you see the back of the weld turning blue or brown, reduce heat or increase travel speed.
3. Improve Fit-up And Joint Preparation
Loose joints or gaps let air reach the hot weld root. Tight, clean fit-up stops this.
- Use clamps or tack welds to hold pieces tight
- Clean edges with a grinder or file—no rust or oil
- Avoid wide root openings (ideally less than 1/16″ or 1.6mm)
Example: On a pipe, if the gap is too wide, even good purging can fail. Air finds its way to the root, causing sugaring.
4. Choose The Right Shielding Gas
Argon is the best choice for TIG welding stainless. Some welders add a small amount of hydrogen (2-5%) for special jobs, but for most work, pure argon is safest.
- Do not use CO₂—it causes oxidation
- Do not use oxygen blends—they destroy the weld
For back purging, only use high-purity argon.
Data Table: Common Shielding Gases for Stainless TIG Welding
| Gas Type | Main Use | Sugaring Risk |
|---|---|---|
| Argon | Main torch and back purge | Very low |
| Argon + 2% Hydrogen | Special thin work | Low (if purged well) |
| CO₂ or O₂ blends | MIG welding (not TIG) | High |
5. Use Trailing Shields And Purge Blocks
For flat welds or large plates, you can use a trailing shield behind the torch. This device floods extra argon on the weld as it cools. For pipes or tight spaces, purge blocks or custom dams help keep argon where you need it.
- Trailing shields snap onto the torch and spread gas wider than the normal cup
- Purge blocks are simple blocks or channels that hold argon under the weld
Example: Welding a long seam on a stainless tank, a welder uses a trailing shield. The weld stays silver, no sugaring appears.
6. Keep Surfaces Clean
Oil, grease, paint, or even fingerprints can burn during welding, making sugaring worse.
- Clean with acetone or alcohol before welding
- Use a stainless brush (not steel) for cleaning edges
- Wear clean gloves to avoid adding oils
Non-obvious Insight: Even small amounts of shop dust or old grinding wheel particles can cause local sugaring. Always use dedicated tools for stainless steel.
7. Control The Environment
Wind, drafts, or fans can blow away shielding gas. Welding outdoors or near open doors increases sugaring risk.
- Block drafts with screens if possible
- Weld indoors or in controlled areas for best results
Example: Welding near a fan, a worker notices the back of the weld turns gray and rough. After moving away from the fan, the welds stay clean.
8. Choose The Right Filler Rod
Use a filler rod that matches the base metal. For 304 stainless, use ER308L. For 316, use ER316L. Mismatched rods can increase oxidation.
- Low-carbon (L) rods reduce carbide precipitation, which can worsen corrosion and sugaring
Non-obvious Insight: Old or rusty filler rods can add contamination. Always store rods in sealed containers.
9. Let The Weld Cool Under Shielding Gas
Stopping gas flow too early lets air hit the hot metal. Keep the gas flowing for a few seconds after you finish welding.
- Use a post-flow setting on your TIG machine (5-15 seconds)
- Do not remove the torch or stop the purge until the weld is cool to the touch
Practical Tip: For thick welds, you may need longer post-flow times.
10. Use Purge Paper, Tape, Or Clay For Sealing
To keep purge gas in and air out, seal open ends tightly.
- Purge paper burns away after welding, but holds gas during the weld
- Aluminum tape works well for flat pieces
- Clay or foam dams can fit odd shapes
Caution: Do not use materials that melt or burn easily, as they can contaminate the weld.
11. Monitor Oxygen Levels
For critical welds, use an oxygen analyzer to check the purge quality. Aim for less than 0.1% oxygen (1,000 ppm) before starting.
- High oxygen means more risk of sugaring
- Simple handheld meters are available for this purpose
Example: In food-grade pipe welding, inspectors check oxygen levels before any weld. Shops reject welds above the set limit.
12. Understand The Impact Of Stainless Steel Types
Some stainless steels are more sensitive to sugaring. For example, austenitic types (like 304, 316) are most common and react quickly with air at high heat. Ferritic and duplex steels can behave differently.
- Thinner steels are more prone to sugaring because they heat up faster
- Higher-alloy steels may need more careful purging
Data Point: 304 stainless starts to oxidize at around 900°C (1650°F) if exposed to air.
13. Check For Leaks And Purge Failures
Even small leaks ruin your purge. Always check:
- Joints
- Seals
- Tape edges
- Fittings
Use soapy water to find leaks—bubbles mean gas is escaping.
Practical Example: A welder finds a small hissing sound at the dam. Fixing it stops sugaring on the next weld.
14. Use Proper Torch Angle And Distance
The torch should aim at the joint, not away from it. A steep angle can pull in air.
- Keep the cup close to the weld pool (1/8″–1/4″)
- Use a larger cup for wider coverage if needed
Tip: Some welders use a gas lens to make the shielding gas flow smoother and wider.
15. Practice Good Welding Technique
Steady hands, even movement, and correct arc length all help reduce oxidation.
- Do not hold the arc too long in one spot
- Keep the filler rod inside the gas shield
- Do not touch the tungsten to the work
16. Learn From Common Mistakes
Many welders repeat the same errors. Some common mistakes:
- Not purging long enough before welding
- Using too high amperage for thin metals
- Rushing the setup and missing leaks
- Not checking the gas type or flow rate
Real-World Example: A shop switched from CO₂ to argon for back purging. Their sugaring problem disappeared.
17. Test And Inspect Your Welds
Look at both sides of your weld. The front might look perfect, but the back can still show sugaring.
- Use a mirror, boroscope, or inspect removable caps to check the back side
- Practice on scrap to fine-tune your purge and technique
Non-obvious Insight: On some pipe welds, a flashlight inside the pipe helps you see sugaring before moving to the next joint.
Comparing Sugaring Prevention Methods
Here’s a summary of the main ways to stop sugaring and how effective they are for different situations:
| Prevention Method | Best For | Effectiveness | Cost |
|---|---|---|---|
| Back Purging (Argon) | Pipe, tubing, food/medical welds | Very High | Moderate |
| Trailing Shield | Long seams, flat plates | High | Low to Moderate |
| Post-Flow Gas | All TIG welds | Medium | Low |
| Clean Fit-Up | All joints | Medium | Low |
| Gas Lens | Critical welds, tight spots | Medium | Low |
| Oxygen Monitor | High-spec jobs | Very High | High |

Credit: www.youtube.com
Special Tips For Different Welding Situations
Welding Thin Stainless Steel
Thin stainless (less than 2mm) is the hardest to protect from sugaring. It heats up and oxidizes fast.
- Use low amperage and move quickly
- Double-check fit-up, as even small gaps matter more
- Back purge is a must
Welding Tubing And Pipes
Pipe welds often need perfect inside surfaces for hygiene and flow.
- Always seal both ends before purging
- Use purge dams or foam to save on argon
- For orbital welding, automated purge systems work best
Field Welding Vs. Shop Welding
Welding outdoors or on-site brings more risk.
- Protect from wind and dust
- Use portable purge kits
- Consider using a mirror to inspect weld roots if you cannot open the pipe
How To Set Up A Simple Back Purge System
You do not need expensive tools to set up a basic back purge:
- Seal the ends of your pipe or joint with tape, clay, or caps
- Drill a small hole in one end for argon in, and one for gas out (vent)
- Connect a hose from your argon regulator to the inlet
- Purge the space until you reach low oxygen
- Weld, keeping the purge on the whole time
- Let cool before removing seals
Real Example: For a 2-inch stainless pipe, 8 CFH of argon for 2-3 minutes usually brings oxygen low enough to weld cleanly.

Credit: primeweld.com
What Happens If You Ignore Sugaring?
Sugaring is not just about looks. It can cause:
- Weld failure in pressure pipes or tanks
- Rusting where you expect stainless to stay clean
- Contamination in food, chemical, or water systems
- Rejected work that costs time and money
In regulated industries, sugared welds can mean big fines or shutdowns. Even in home projects, ignoring sugaring leads to repairs and lost confidence in your work.
How Do Professionals Check For Sugaring?
- Visual inspection: Mirrors, flashlights, and cameras
- Borescope: For small pipes or sealed systems
- Weld coupons: Test pieces cut open to check root quality
- X-ray: For critical welds in pipelines
Most shops use a mix of these, depending on the job.
Real-world Example: Food-grade Welding
In a dairy processing plant, welders must pass strict tests. Each weld is checked for sugaring with a mirror and flashlight. Any sign of gray or black oxide means the weld is cut out and replaced.
The shop uses argon back purging, oxygen monitoring, and trailing shields to keep welds bright. Welders clean with alcohol and use only stainless brushes. Their rejection rate dropped from 20% to under 2% after making these changes.
Frequently Asked Questions
What Causes Sugaring When Tig Welding Stainless Steel?
Sugaring happens when the hot back side of a stainless weld touches air. The high heat reacts with oxygen, making rough oxides. Not enough purge gas, too much heat, or poor fit-up are common causes.
Can You Remove Sugaring After Welding?
You can grind or sand off the oxide, but this does not fix the metal below. The weld may still be weak or more likely to rust. Prevention is better than repair.
What Is The Best Gas For Back Purging Stainless Steel?
Argon is the best gas for back purging. It is inert and does not react with hot metal. Use high-purity argon for best results. Do not use CO₂ or oxygen mixes.
How Much Argon Flow Do I Need For Back Purging?
For small pipes, 5-10 CFH is enough. For large spaces, use 15-20 CFH or more. Always adjust flow to fill the space without wasting gas.
Do All Stainless Steels Sugar The Same Way?
No. Austenitic grades like 304 and 316 sugar easily. Ferritic and duplex steels react less, but can still sugar if not protected. Thinner and higher-alloy stainless are more sensitive.
For more technical details, you can check the Wikipedia TIG welding page.
Stopping sugaring when TIG welding stainless steel takes planning, good technique, and the right equipment. Once you master these steps, your welds will be clean, strong, and ready for any inspection or use.
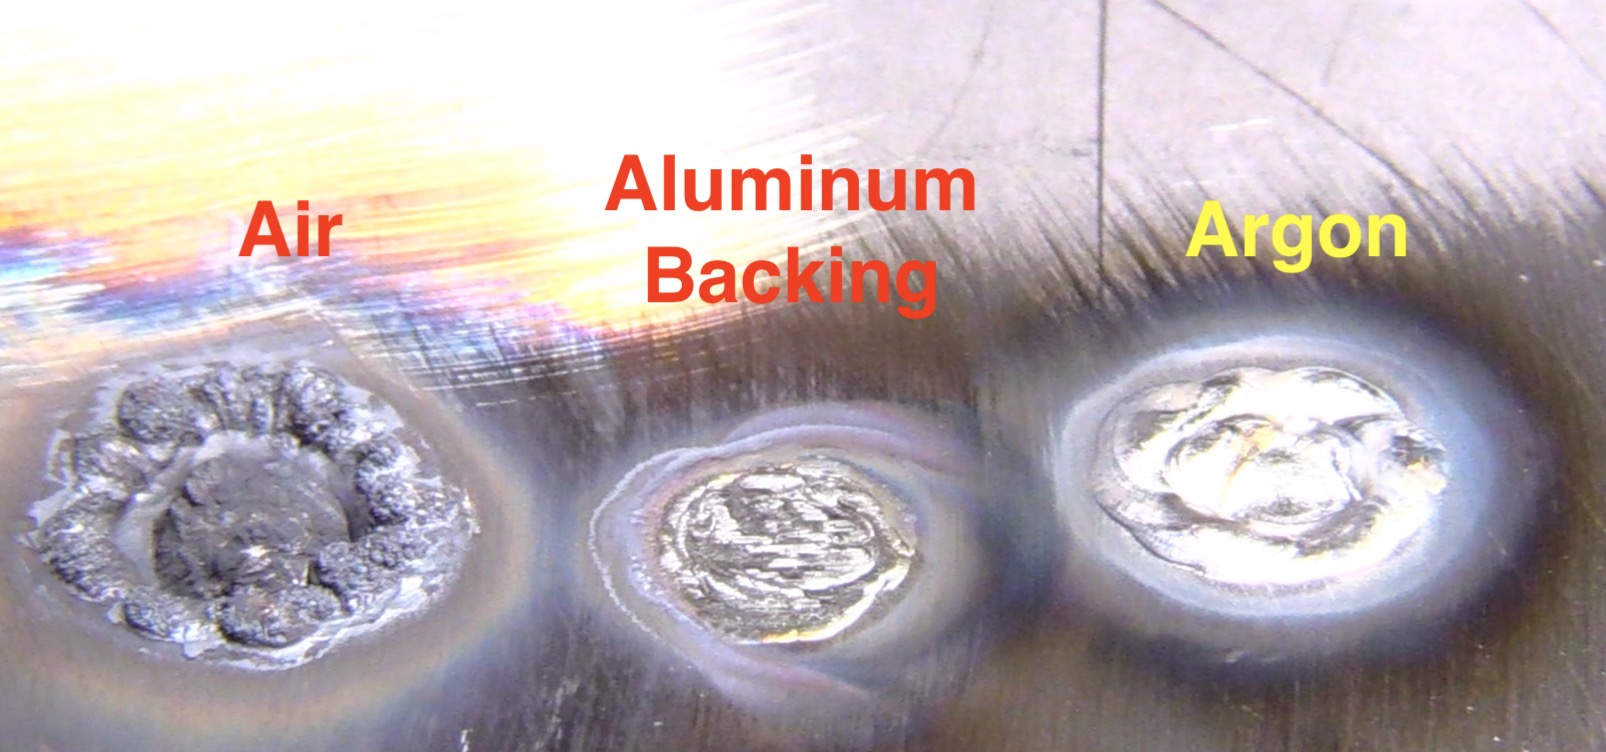
Credit: www.weldingtipsandtricks.com