Disclosure: This post contains affiliate links and I will be compensated if you make a purchase after clicking through my links. Learn More
The numbers on a welding rod, such as 6011 or 7018, reveal critical details: tensile strength, welding position, flux type, and current compatibility. Understanding these numbers helps you pick the right rod for strong, safe, and reliable welds every time. Even though the rod just looks like a coated stick, its code tells you exactly what it’s made for. If you want strong welds that won’t fail, you need to know what each number means and why it matters.
Why Welding Rod Numbers Matter
Welding rods are more than just sticks of metal. Each rod type is designed for specific jobs. The numbers printed on a rod, like E6011 or E7018, are not random. They act as a code, telling you exactly what that rod can do. If you ignore these numbers, you risk weak welds, costly repairs, or safety hazards. For example, using a rod made for flat welds on a vertical surface can cause the weld to sag or even break. If you choose a rod with the wrong flux, you might end up with a dirty weld that is hard to clean or even full of holes.
Knowing how to read welding rod numbers means you can work with confidence, avoid mistakes, and deliver strong results. It also helps you troubleshoot problems. For instance, if your welds keep cracking, checking the rod numbers might reveal you’re using a rod with the wrong hydrogen level.
In professional settings, inspectors will check if you used the right rod for the job—so understanding these numbers can protect your reputation and your paycheck.
Breaking Down The Welding Rod Number System
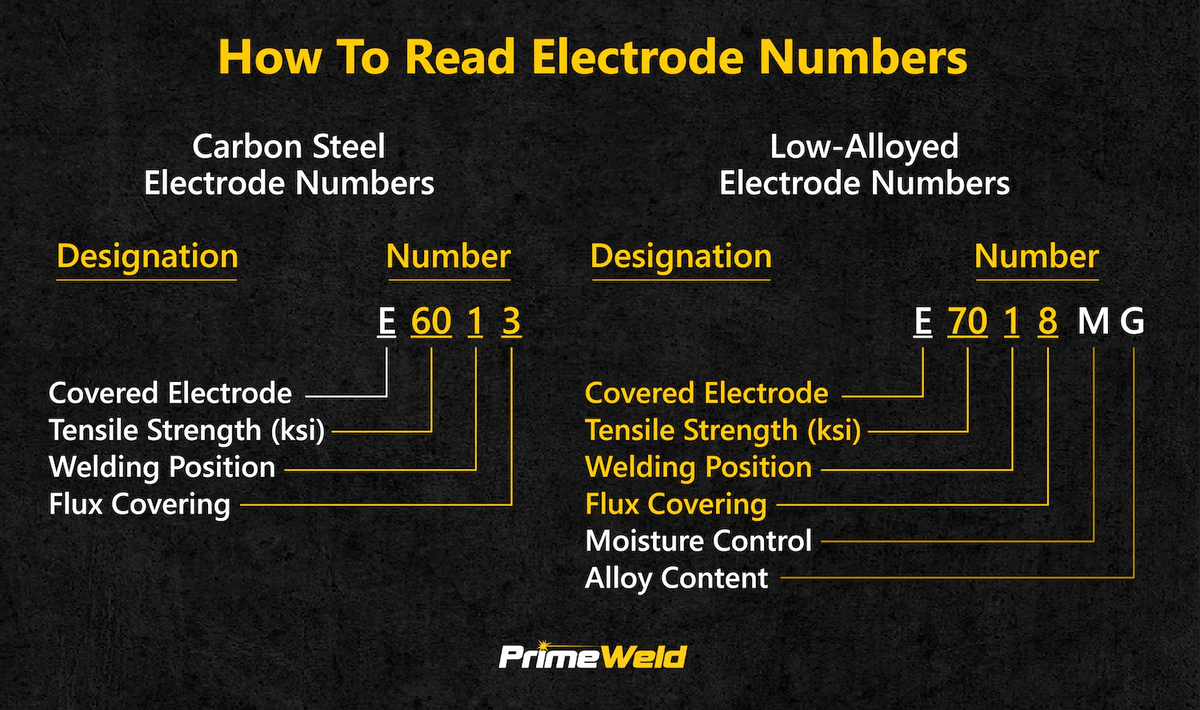
Most stick welding rods use a system set by the American Welding Society (AWS). You’ll usually see a letter “E” followed by four or five numbers. For example: E7018.
Here’s what each part means:
- E stands for “electrode” (the welding rod itself).
- The first two or three numbers show the rod’s minimum tensile strength in thousands of pounds per square inch (psi).
- The next number tells you what positions you can weld in.
- The last number describes the flux coating and which current (AC, DC, or both) the rod uses.
Let’s break that down further.
Example: Reading E6011
- E = Electrode
- 60 = 60,000 psi tensile strength
- 1 = All positions (flat, vertical, overhead, horizontal)
- 1 = Cellulosic coating, AC or DC current
So, E6011 is a rod that is strong enough for most repair jobs, works in any position, and can be used with almost any welder.
Example: Reading E7018
- E = Electrode
- 70 = 70,000 psi tensile strength
- 1 = All positions
- 8 = Low-hydrogen coating, AC or DC+ current
E7018 is popular in construction because it’s strong, flexible for any welding position, and makes clean, low-hydrogen welds that resist cracking.
Knowing these basics helps you choose the best rod for the job. For example, if you’re fixing a gate at home, you might pick E6011 because it can handle dirty metal and basic machines. If you’re building a steel frame for a building, you want E7018 for its higher strength and reliable performance.
Credit: weldingmart.com
Understanding Each Part Of The Number
1. The “e” Means Electrode
Every stick welding rod starts with an E. This letter simply means the rod is an electrode, which conducts electricity to melt and join metal. It’s a reminder that the rod is not just a filler—it’s an active part of the welding process. Whether you’re using a small portable welder or a big industrial machine, the “E” ensures you’re using the right consumable for stick welding.
2. Tensile Strength
The first two or three numbers show the rod’s tensile strength—how much force the weld can handle before breaking. For example, a “60” means 60,000 psi, “70” means 70,000 psi. Higher numbers mean stronger welds. If you’re working on structures that must hold heavy loads, choose rods with higher tensile strength.
As a practical example, E7018 is often chosen for bridges and skyscrapers because engineers trust its 70,000 psi weld strength. On the other hand, E6013 is fine for making a gate or repairing a lawn mower, since 60,000 psi is more than enough.
Choosing the right strength means your weld won’t be the weak point in your project.
3. Welding Position
The third number tells you which positions are safe for welding:
- “1” = All positions (flat, vertical, overhead, horizontal)
- “2” = Flat and horizontal only
Rods marked with a “1” are more flexible for complex jobs. For example, if you have to weld something that can’t be moved or rotated, a “1” rod is your best friend. If you use a “2” rod on a vertical joint, the molten metal can drip or sag because the coating isn’t designed for those positions.
4. Flux Coating And Current
The last number tells you about the flux coating and what type of electric current you need:
- “0” = High cellulose sodium, DC only
- “1” = High cellulose potassium, AC or DC
- “2” = High titania sodium, AC only
- “3” = High titania potassium, AC or DC
- “4” = Iron powder, titania, AC or DC
- “5” = Low hydrogen sodium, DC only
- “6” = Low hydrogen potassium, AC or DC
- “8” = Low hydrogen iron powder, AC or DC+
This number is key for matching the rod to your welding machine. For example, if you have a simple AC “buzz box” welder, you need rods ending in “1” or “3. ” If you try to run a “0” or “5” rod, the arc may not start, or the rod will just stick to the metal.
The flux type also affects how much smoke, splatter, and slag you get, as well as how easy it is to clean the weld.
Most Common Welding Rods And Their Numbers
Some rods are used more often than others in workshops and construction sites. Each has its own strengths and best uses. Choosing the right one saves time and avoids headaches.
E6010
- Strength: 60,000 psi
- Position: All
- Coating: Cellulosic sodium, DC only
- Best for: Piping, root passes, deep penetration
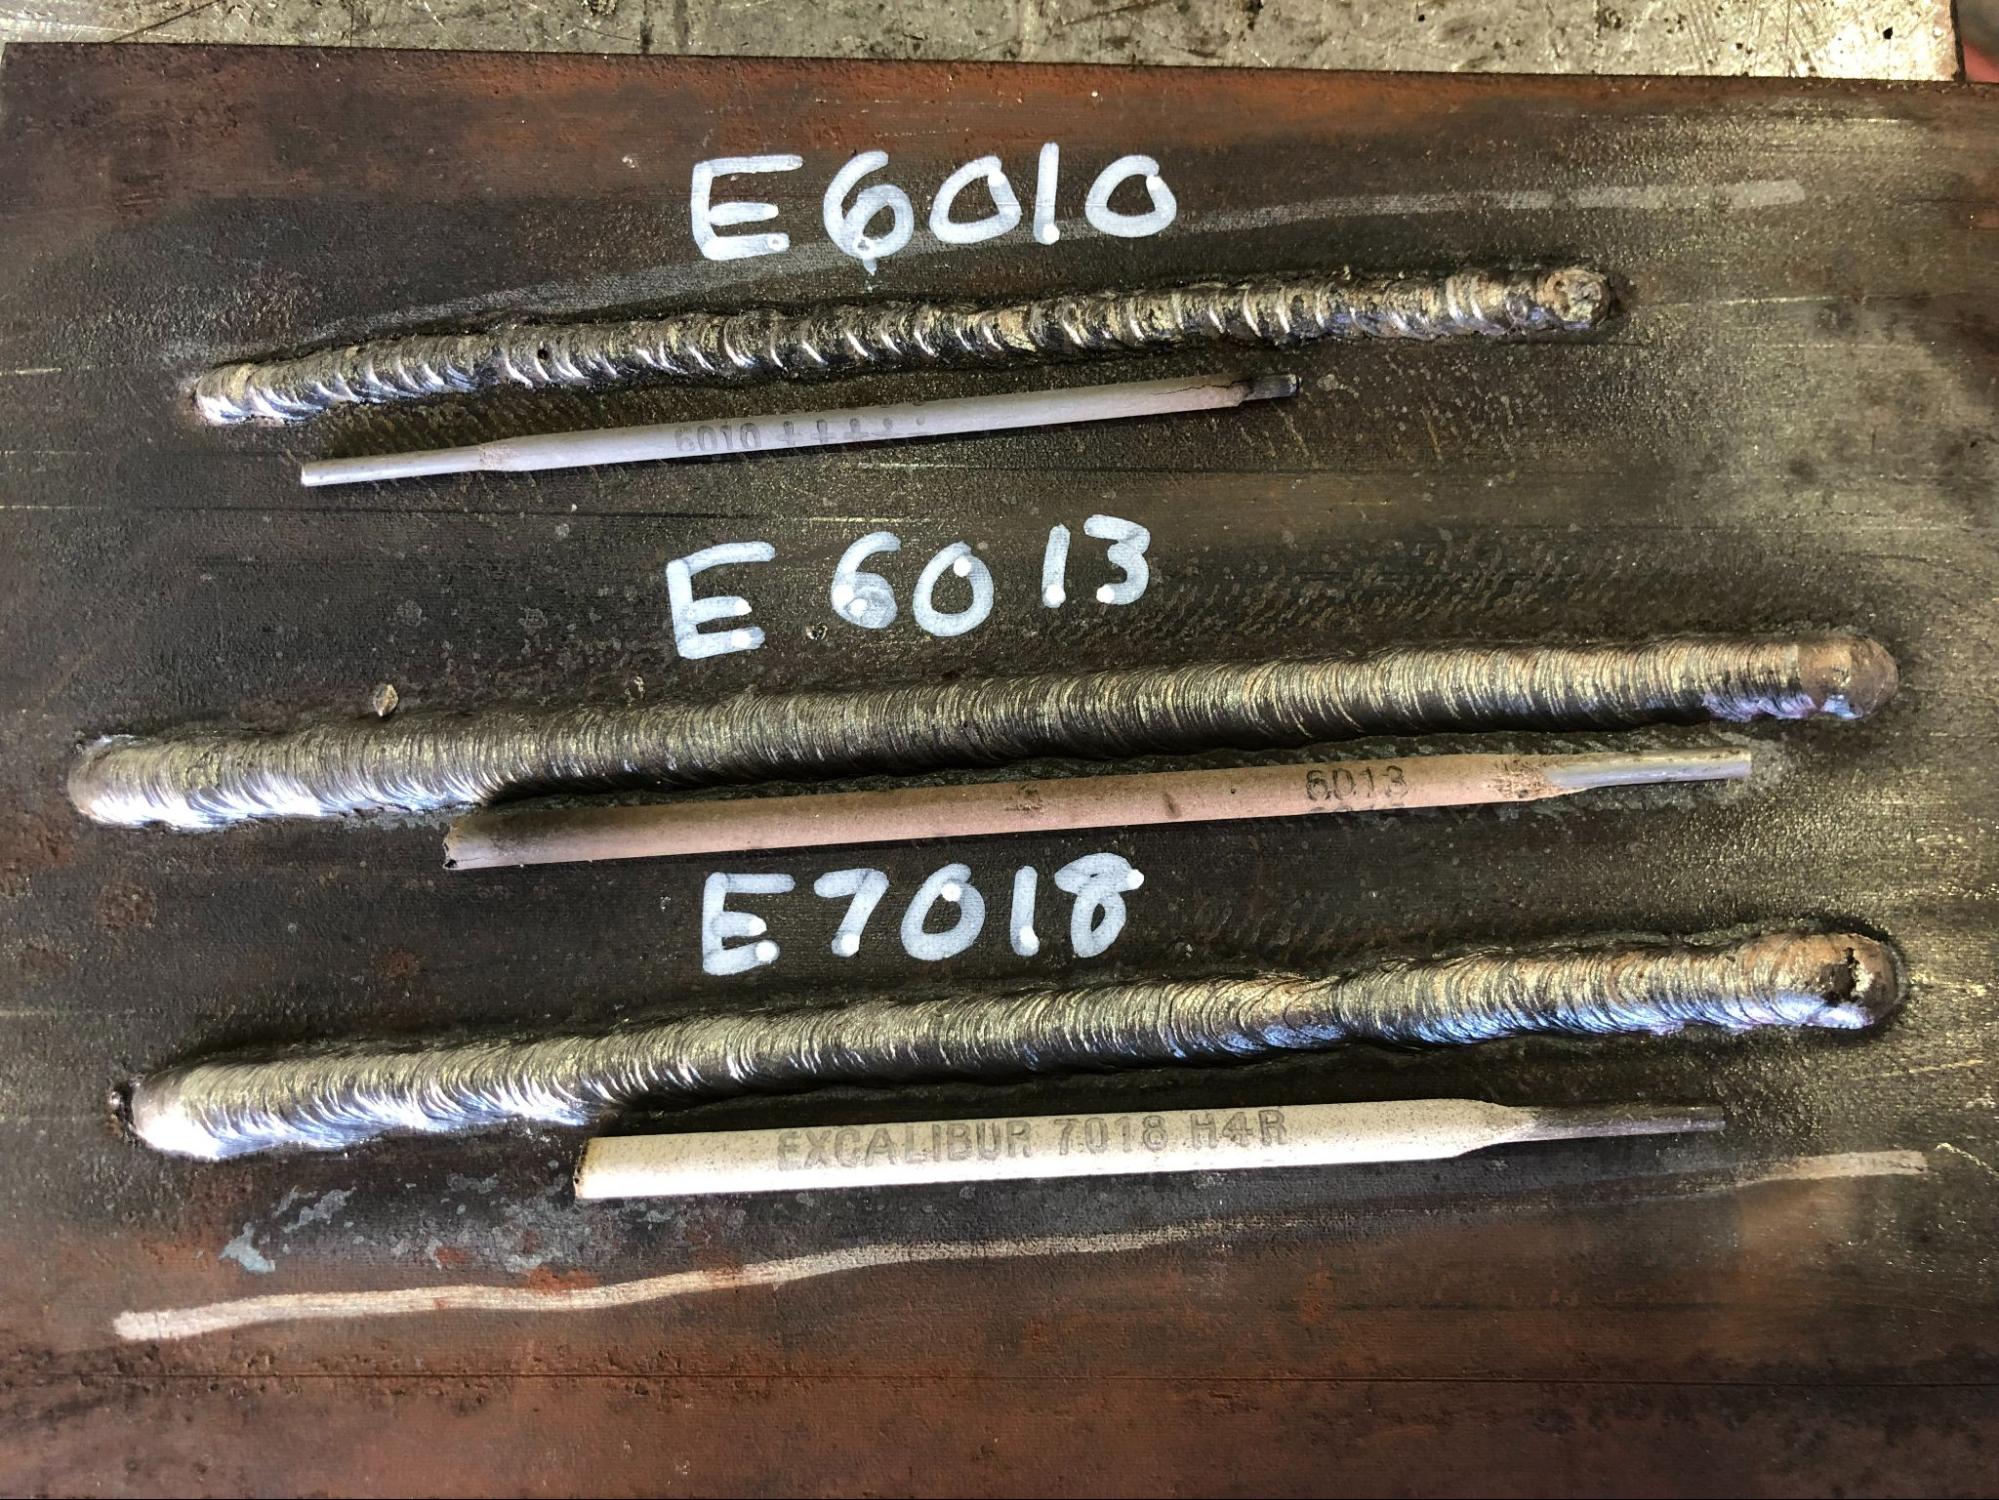
E6010 is common in pipe welding because it can dig through rust, paint, and even some grease. It’s also great for the first pass on a joint (root pass) because it penetrates deep into the metal.
E6011
- Strength: 60,000 psi
- Position: All
- Coating: Cellulosic potassium, AC or DC
- Best for: Dirty/rusty steel, farm repairs, deep penetration
E6011 is the rod of choice for farmers and field repairs. It works even if you can’t clean the metal perfectly, and it’s very forgiving if your machine is old or basic.
E6013
- Strength: 60,000 psi
- Position: All
- Coating: Titania potassium, AC or DC
- Best for: Thin metals, smooth welds, general repairs
E6013 is great for beginners. It strikes an arc easily, creates a smooth bead, and the slag (the leftover coating) comes off with just a brush. It’s perfect for welding car panels, sheet metal boxes, or small projects.
E7014
- Strength: 70,000 psi
- Position: All
- Coating: Iron powder titania, AC or DC
- Best for: Fast fill, thick joints, smooth finish
E7014 is used when you want to fill big gaps quickly. It’s often used in fabrication shops where speed matters, and the iron powder in the coating helps deposit more metal in less time.
E7018
- Strength: 70,000 psi
- Position: All
- Coating: Low hydrogen iron powder, AC or DC+
- Best for: Structural welding, critical joints, code work
E7018 is the “gold standard” for code welding. It’s required for bridges, buildings, and places where weld failure is not an option. Its low-hydrogen coating stops cracks and makes it safe for thick, critical joints.
E7024
- Strength: 70,000 psi
- Position: Flat and horizontal
- Coating: Iron powder titania, AC or DC
- Best for: High-speed, large flat welds, heavy plate
E7024 is a production rod—used to quickly lay down big welds on thick, flat steel. It’s not for overhead or vertical welding, but for jobs like making railings or beams, it’s hard to beat.
How To Choose The Right Welding Rod
Picking the right rod isn’t just about reading numbers. You need to think about:
- Metal type: Mild steel, stainless, cast iron, etc.
- Welding position: Overhead, vertical, or flat?
- Welding machine: AC, DC, or both?
- Joint design: Thin sheet or thick plate?
- Work conditions: Dirty, painted, or rusty metal?
Let’s look at some practical examples.
Scenario 1: Welding Rusty Farm Equipment
- Best choice: E6011 rod
- Why: It works with AC or DC, penetrates rust, and handles dirty surfaces. Even if you only have a small farm welder, E6011 gets the job done without perfect prep.
Scenario 2: Building A Trailer Frame
- Best choice: E7018 rod
- Why: High strength, low hydrogen (prevents cracking), works in all positions, good for critical welds. If you want your trailer to last, E7018 is a smart choice.
Scenario 3: Quick Home Repairs
- Best choice: E6013 rod
- Why: Easy to use, smooth welds, works on thin metal. For fixing a mailbox, garden tools, or small brackets, E6013 makes clean welds with little effort.
One detail beginners miss: sometimes the “easiest” rod isn’t the best. For example, E6013 is easy, but it doesn’t penetrate as deeply as E6011 or E7018. If you need to weld thick, rusty steel, E6011 might be better—even if it’s a little harder to use.
Key Insights Most Beginners Miss
- Last Number Impacts Weld Quality: Many new welders focus on tensile strength and ignore the last digit. But flux coating (last number) affects everything—arc stability, penetration, and even cleanup time. For example, “8” rods (like E7018) create less spatter and smoother beads, but require dry storage. “1” rods (like E6011) handle dirt and rust, but make more smoke.
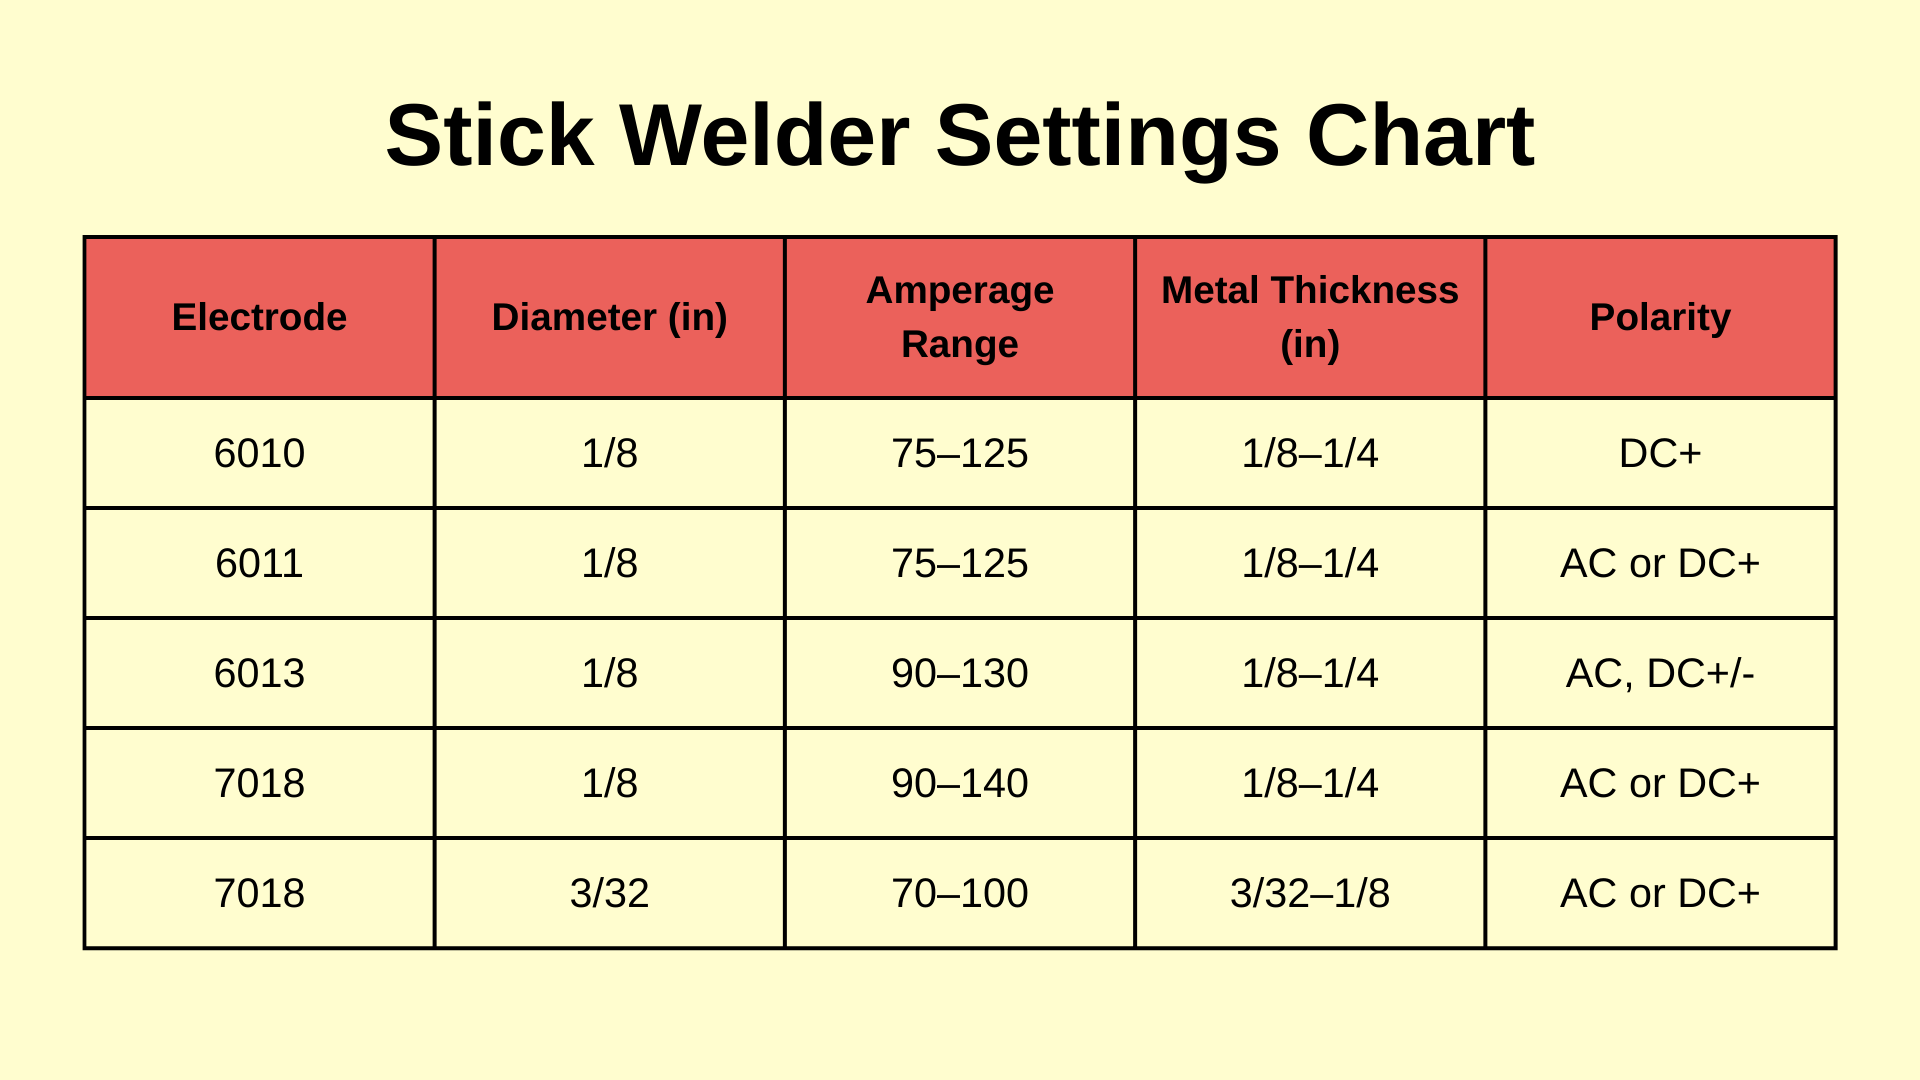
- Current Compatibility: Not all rods work with every welding machine. For example, E6010 won’t run on AC, so if you use a basic AC welder, you need E6011 or E6013. This is a common mistake for beginners—they buy a “strong” rod but can’t get it to work.
- Storage Matters: Low-hydrogen rods like E7018 absorb moisture fast. Wet rods can cause weld defects. Always keep them in a rod oven or sealed container.
- Matching Rod to Base Metal: If you try to weld stainless steel with a normal E6013 rod, the weld will rust and fail. Always match the rod’s chemistry to the metal.
- Don’t Overlook Position Number: Using a “2” position rod for anything except flat or horizontal welds leads to poor, saggy welds.
Credit: openwa.pressbooks.pub
Detailed Comparison: Popular Welding Rods
Below is a side-by-side look at the most used welding rods. This helps you decide faster.
| Rod Type | Tensile Strength (psi) | Welding Position | Coating Type | Current | Main Use |
|---|---|---|---|---|---|
| E6010 | 60,000 | All | Cellulosic sodium | DC | Pipes, root pass |
| E6011 | 60,000 | All | Cellulosic potassium | AC/DC | Dirty/rusty steel |
| E6013 | 60,000 | All | Titania potassium | AC/DC | Thin metal, clean welds |
| E7018 | 70,000 | All | Low hydrogen iron powder | AC/DC+ | Structural, code welds |
| E7024 | 70,000 | Flat, horizontal | Iron powder titania | AC/DC | Heavy, flat welds |
The Meaning Of Each Flux Coating (last Digit)
The flux is a special coating on the outside of the rod. It protects the weld from contamination and affects how the rod performs. Here’s what each last digit means in detail:
Last Digit “0” Or “1”
- 6010: High cellulose sodium, deep penetration, DC only. Good for pipeline welding.
- 6011: High cellulose potassium, deep penetration, works with AC or DC. Chosen for repairs in the field.
These rods make a strong, forceful arc that can burn through rust, paint, and dirt. They are best for root passes and first layers.
Last Digit “2” Or “3”
- 6012: High titania sodium, AC only, for high-speed welds on thin plate.
- 6013: High titania potassium, AC or DC, smooth arc, easy slag removal.
These rods make a softer arc and are best for sheet metal and home projects. They don’t dig as deep but leave a neat weld.
Last Digit “4”
- 7014: Iron powder titania, AC or DC, fast fill, high deposition rate.
“4” rods are good for building up thick welds quickly, especially on horizontal or flat joints.
Last Digit “5,” “6,” Or “8”
- 7015: Low hydrogen sodium, DC only, for critical welds.
- 7016: Low hydrogen potassium, AC or DC, resists cracking.
- 7018: Low hydrogen iron powder, AC or DC+, excellent for structural work.
“8” rods combine high strength with a smooth arc, but must be kept dry to prevent weld cracking. They’re chosen for code work and heavy structures.
The choice of rod impacts how you weld, not just the result. The wrong flux can make a job take longer, look worse, or even fail inspection.
Welding Rod Number Chart For Quick Reference
This chart helps you quickly match rod numbers to their main features:
| Rod Number | Tensile Strength | Welding Position | Coating | Current | Common Use |
|---|---|---|---|---|---|
| E6010 | 60,000 psi | All | Cellulosic sodium | DC | Pipelines, root passes |
| E6011 | 60,000 psi | All | Cellulosic potassium | AC/DC | Maintenance, repair |
| E6013 | 60,000 psi | All | Titania potassium | AC/DC | Sheet metal, home repairs |
| E7018 | 70,000 psi | All | Low hydrogen iron powder | AC/DC+ | Bridges, buildings |
| E7024 | 70,000 psi | Flat, horizontal | Iron powder titania | AC/DC | Heavy plate, production |
What Happens If You Pick The Wrong Rod?
Choosing the wrong rod can cause serious problems:
- Weak welds that break under pressure
- Cracks in the metal, especially on critical joints
- Porosity (tiny holes) from moisture or wrong flux
- Poor penetration if the rod isn’t strong enough
- Hard starts or sticking if the rod isn’t compatible with your welder
Some problems aren’t obvious right away. For instance, moisture in E7018 rods can cause hydrogen cracks that appear days or weeks after welding. If you use a “2” position rod for a vertical weld, the bead may look fine at first, but it can fail with vibration or heavy load.
Using the right rod means you’re not just hoping for a good weld—you’re sure of it.
Welding Rods For Special Applications
Not all jobs use common rods. Some projects need special types:
- Stainless steel rods: Numbered like E308, E309, or E316. For welding stainless steel.
- Cast iron rods: Numbered as ENi-CI or similar. For cracked or broken cast iron.
- Hardfacing rods: For wear-resistant coatings on tools, blades, or buckets.
Each special rod has its own number system, but the main AWS code principle stays the same. For example, E308 means “Electrode, 308 stainless steel alloy. ” These special rods cost more, but using the correct type prevents rust, cracking, or early failure of the weld.
Tips For Storing And Handling Welding Rods
- Keep rods dry. Low-hydrogen rods like E7018 must be stored in a rod oven at 250°F-300°F (120°C-150°C).
- Seal opened packages. Use airtight containers or reseal bags to keep moisture out.
- Don’t mix rod types. Even if they look similar, mixing can cause weld problems.
- Check expiration dates. Some rods lose effectiveness over time, especially low-hydrogen types.
Moisture ruins rods by causing hydrogen-induced cracking. This can destroy critical welds and cost you time and money. In humid climates, rods can absorb water in just a few hours, so always reseal or bake rods as needed. For most home users, simple plastic tubes with tight caps work well for short-term storage.
Common Mistakes To Avoid
- Ignoring the last digit. Many beginners just look at tensile strength and welding position, but the last number controls arc characteristics and cleanup.
- Using E6010 on AC welders. E6010 only works with DC. If you use AC, the arc will be unstable.
- Not matching rod to base metal. Stainless, cast iron, and mild steel rods are not interchangeable.
- Welding out of position. Using a rod meant for flat welds on a vertical job leads to poor results.
- Not storing rods correctly. Moisture is the silent killer of good welds, especially with E7018.
Another common mistake is using a “stronger” rod when it’s not needed. Higher strength rods, like E7018, are harder to use and require more care (like dry storage). If your project doesn’t need that strength, a simpler rod like E6011 or E6013 will make welding easier and faster.
Practical Examples: Real-world Rod Selection
Repairing A Rusty Trailer
- Best rod: E6011
- Reason: Penetrates rust, works with basic AC welders, easy to use outdoors. You don’t have to grind every bit of rust or paint away.
Welding A Steel I-beam For A Building
- Best rod: E7018
- Reason: High strength, low hydrogen, meets building codes, works in all positions. Inspectors look for this rod in structural work.
Fabricating Sheet Metal Boxes
- Best rod: E6013
- Reason: Smooth arc, doesn’t burn through thin steel, easy to control. You get neat, clean welds without warping the metal.
Heavy Equipment Hardfacing
- Best rod: Hardfacing rod (not E60XX/E70XX)
- Reason: Designed for wear resistance, not just strength. Hardfacing rods add a tough surface to plow blades, buckets, or crushers.
Choosing Between 6010, 6011, 6013, 7014, And 7018
Each rod has a sweet spot. Here’s a direct comparison:
- 6010: Deep penetration, DC only, best for pipe and root passes.
- 6011: Deep penetration, AC or DC, best for field repairs.
- 6013: Smooth weld, easy to use, best for thin metals.
- 7014: Fast fill, high deposition, best for horizontal/flat welds.
- 7018: High strength, all position, best for structural and code work.
If you’re not sure, ask yourself: Is the metal clean or dirty? Is it thick or thin? Do I need a weld that passes inspection? Your answers will point to the right rod.
How The Right Rod Boosts Productivity
A proper rod cuts welding time, reduces rework, and ensures safety. For example, using E7018 on structural steel means fewer callbacks and inspections passed the first time. E6011 on dirty steel saves hours of grinding and cleaning.
The right rod also improves weld appearance. For example, E6013 gives a smooth, shiny bead on car panels, while E7018’s low spatter makes it easier to grind and paint. If you pick a rod that matches your machine and skill level, you’ll spend more time welding and less time fixing problems.
Industry Data: Welding Rod Usage In The Usa
- Over 60% of structural welds in the USA use E7018 due to its strength and low-hydrogen properties.
- E6011 is the top choice for farm and field repairs because of its versatility and tolerance for dirty surfaces.
- E6013 is popular in hobby shops and schools for its ease of use.
Quick Recap: How To Read Welding Rod Numbers
- First two (or three) digits: Tensile strength (in 1,000 psi)
- Third digit: Welding position (1 = all, 2 = flat/horizontal)
- Last digit: Flux type, current compatibility, arc characteristics
If you understand these, you can pick the right rod every time. Even if you forget the details, just remember: the numbers are a code, and the code tells you everything you need to know for safe, strong welds.
Frequently Asked Questions
What Does The “e” Mean In Welding Rod Numbers?
The “E” stands for electrode. It means the rod conducts electricity to the weld. Every stick welding rod starts with an “E” to show it’s the part that creates the arc and melts to form the weld.
Can I Use E6011 Instead Of E6010?
Yes, you can use E6011 instead of E6010, especially if you have an AC welder. E6011 works with both AC and DC, while E6010 is DC only. Both provide deep penetration on dirty or rusty steel.
Why Is E7018 Used For Structural Welding?
E7018 is used for structural welding because of its high tensile strength (70,000 psi) and low-hydrogen coating. This reduces the risk of cracking and meets building codes, making it ideal for bridges and buildings.
Credit: www.arccaptain.com
What Happens If Welding Rods Get Wet?
Wet welding rods, especially low-hydrogen types like E7018, can cause weld defects such as porosity or cracking. Moisture in the coating creates hydrogen, which weakens the weld. Always store rods in a dry, sealed container or rod oven.
How Do I Know Which Welding Rod To Use?
Check the metal type, welding position, and your machine’s power source. Then read the rod’s numbers: strength, position, and flux type. Use rods like E6011 for repairs, E7018 for structure, and E6013 for thin metal or easy practice.
When you know how to read welding rod numbers, you can weld with total confidence. The right rod makes your work safer, faster, and built to last. Every welder should master this simple code—it’s your shortcut to great results every time.